T: +86-139-5050-9685
E: sales@bycpower.com
E: sales@bycpower.com
No. 13, Jincheng road, Tiehu village, Chengyang town, Fuan city, Fujian, China


Views: 0 Author: Site Editor Publish Time: 2026-10-05 Origin: Site


Taking delivery of a new or refurbished 12 kW generator does not end your procurement cycle. It actually triggers the most critical final validation step. Your facility depends on immediate, reliable backup power to maintain operations during sudden grid outages.
Accepting a unit blindly carries immense operational and financial risks. Concealed transit damage, hidden manufacturing defects, or missing compliance documents can ruin your investment. You cannot afford to discover these catastrophic failures during an actual emergency. Once you sign the shipping receipt unconditionally, shifting the liability back to the carrier or manufacturer becomes extremely difficult.
We will walk you through a rigid, evidence-based receiving protocol. You will learn exactly how to inspect vulnerable exposed components, validate mechanical integrity, and verify real-world load performance. This specific guide protects your warranty and ensures your equipment remains ready to run securely on day one.
Visual inspections must specifically target the exposed vulnerabilities inherent to open-frame designs.
Mechanical and fluid checks should identify micro-leaks or misalignment caused by shipping vibrations.
A comprehensive 12 kW diesel generator quality inspection requires verifiable load bank testing, not just a no-load startup.
Documentation validation (including third-party certifications like SGS reports) is mandatory before signing the bill of lading.
A successful receiving process begins long before the delivery truck arrives. You must establish strict rules for what your facility will accept. Defining your success criteria early prevents panic and confusion on the loading dock. A cosmetic scratch on the base frame might be acceptable. A bent alternator housing or leaking fuel line is an automatic rejection.
You need to differentiate between minor shipping wear and functional damage. Scuffed paint requires a simple note on the bill of lading. Sheared engine mounts indicate severe mishandling. In these cases, you must refuse the delivery entirely to protect your operational readiness.
You must prepare a designated staging area to conduct a safe and thorough inspection. Never inspect a generator while it sits on the back of a moving delivery truck. Move the unit to a staging zone. This area must feature level ground to ensure accurate fluid level readings. It also needs adequate overhead lighting so you can spot hidden stress fractures.
Keep spill containment materials ready. Shipping vibrations can loosen factory seals. You might encounter sudden coolant or oil leaks when you tilt the unit during offloading. A prepared environment keeps your team safe and keeps the inspection organized.
Do not rely entirely on visual checks. You need proper diagnostic equipment to evaluate the internal health of the machine. We recommend preparing a staging cart equipped with specific testing tools. Your inspection team should have immediate access to the following:
Digital Multimeter: Essential for checking battery voltage and continuity.
Vibration Meter: Helps detect unbalanced shafts during the initial test run.
High-Lumen Flashlight: Required to illuminate dark crevices near the oil pan.
Telescoping Mechanic’s Mirror: Allows you to inspect the underside of the alternator and engine block.
Portable Load Bank: Mandatory if you plan to conduct immediate performance testing on the dock.
Common Mistake: Many buyers sign the delivery paperwork before gathering their tools. Always pause the driver. Retrieve your tools and perform the inspection first.
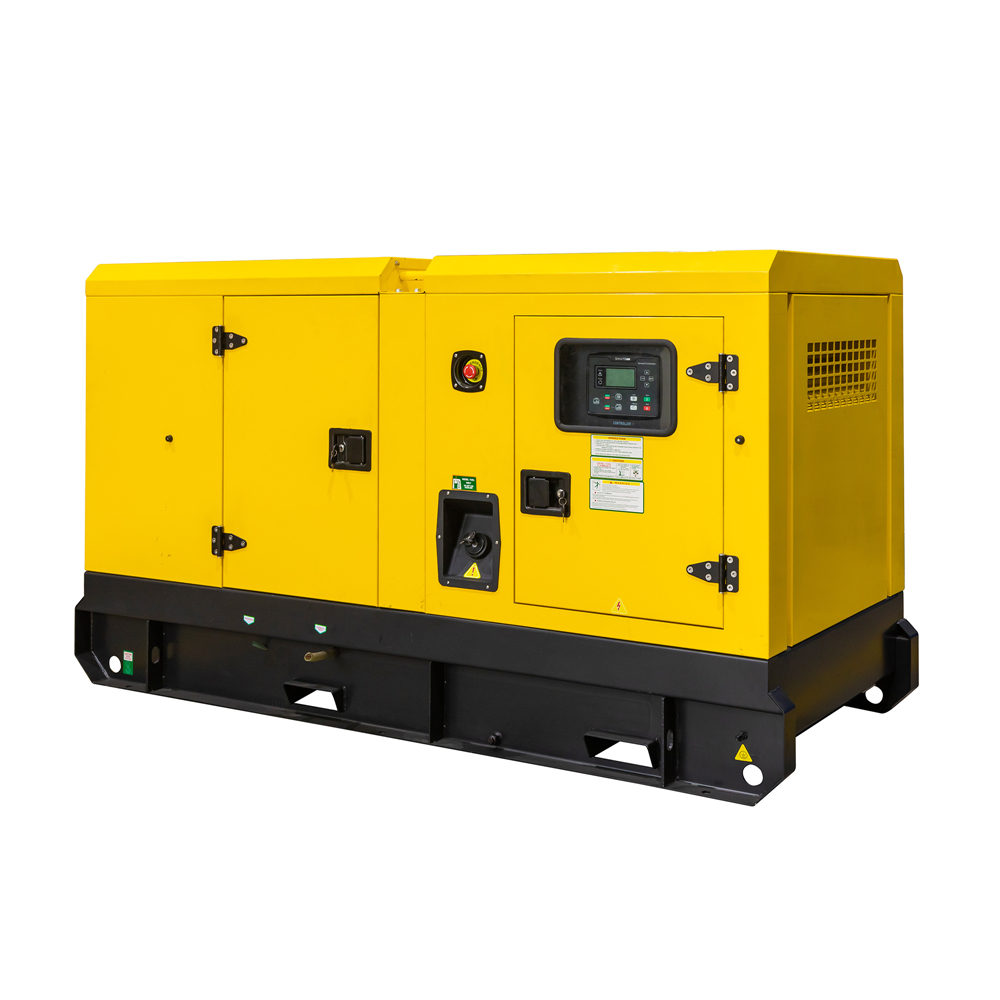
Unlike enclosed units, an open diesel generator lacks a protective outer canopy. This design provides excellent cooling and easy maintenance access. However, it also leaves critical engine and electrical components highly vulnerable during transit. You must scrutinize the physical structure aggressively.
Start your inspection at the foundation. The skid base supports the entire weight of the engine and alternator. Look closely at the forklift pockets and lifting points. Forklift operators frequently misjudge the center of gravity. This mishandling can bend the steel frame or cause hairline stress fractures in the factory welds.
Run your flashlight along all welded seams. If you see chipped paint directly over a weld, it often indicates the metal has flexed beyond its tolerance. A compromised base frame will cause severe engine misalignment over time.
Because the unit lacks shielding, you must meticulously check the delicate external parts. Inspect the radiator fins first. Even a minor bump from a shifting pallet can crush these aluminum cooling fins. Crushed fins restrict airflow and lead to rapid overheating under load.
Next, trace the exposed wiring harnesses. Look for pinch points where wires might have rubbed against the steel frame during transport. Finally, check the unshielded belts for physical impact damage or deep cuts. Replacing a damaged belt now prevents a sudden failure later.
The anti-vibration rubber mounts isolate the intense engine shaking from the rigid base frame. These isolators take significant abuse during cross-country shipping. Verify they remain fully intact. Check for uneven compression. If one rubber mount looks heavily pancaked while the others look normal, the frame might be bent, or the mount has failed.
If your unit is configured as a heavy-duty portable generator, you must evaluate its mobility components. Inspect the wheel axles for straightness. Test the locking casters to ensure they engage and disengage smoothly. Verify the structural soundness of the overhead lifting eyes. You will rely on these points to move the unit safely around your facility.
Shipping vibrations are notorious for loosening factory-tightened mechanical fittings. A machine might leave the assembly line perfectly sealed, only to arrive at your facility leaking vital fluids. You must perform a rigorous mechanical validation before attempting any startup procedures.
Perform a slow, 360-degree walkaround focused entirely on fluid retention. Look for oil, coolant, or diesel micro-leaks. These leaks often start as a slow weep rather than a steady drip. Wipe a clean paper towel under the engine block and oil pan to check for fresh residue.
Pay special attention to all threaded fittings, bottom drain valves, and filter housings. Transport vibration easily backs out improperly torqued drain plugs. If you detect diesel fuel on the skid, do not start the machine. Fuel leaks present a massive fire hazard.
Visually verify the alignment of the rotating assemblies. The cooling fan must sit perfectly centered within the radiator shroud. If the fan blades touch the shroud housing, the engine mounts have likely shifted. Inspect the drive belts and pulleys. They should align perfectly straight. Misaligned pulleys will shred a drive belt within the first few hours of operation.
Engines require unrestricted airflow and steady fuel pressure to generate rated power. Inspect all rubber hoses for pinched, kinked, or abraded sections. A kinked fuel return line will cause erratic engine surging. Ensure the air filter housing seals tightly. Open the housing to verify no shipping debris, like cardboard dust or plastic wrap, has bypassed the filter element.
Never assume the factory filled the fluids to the correct levels. Check the engine oil dipstick. Check the radiator coolant level. Ensure they meet operational baselines. Some manufacturers ship units dry to comply with freight regulations. Starting a dry engine destroys the internal bearings immediately. Always establish this baseline before you touch the ignition switch.
An engine can run flawlessly, but if the electrical controls fail, your facility remains in the dark. The control panel acts as the brain of the machine. You must verify its integrity carefully, as shipping impacts easily dislodge sensitive electronic components.
If the control panel provides safe access, open the rear cover. Inspect the internal wiring blocks. Look for loose terminal screws. Tug gently on the main connection points to ensure they seated properly at the factory. Inspect the external alternator connections. Verify the factory installed the heavy grounding straps securely. A missing ground strap creates a lethal shock hazard for your operators.
Standby power systems rely on the starting battery. Verify the physical condition of the battery case. Look for hairline cracks or acid leaks around the base. Check the terminal tightness. Use your multimeter to verify the standing DC voltage. A healthy 12V system should read around 12.6 to 12.8 volts at rest. If the battery arrives dead, it may indicate a parasitic draw in the control panel.
You must validate the digital logic before starting the engine. Power on the main control module. Do not crank the engine yet. Watch the boot-up sequence on the digital display. Check the event log for any pre-existing error codes triggered during factory testing. Verify the sensor readings. The coolant temperature should match the ambient room temperature. Ensure all display pixels function correctly.
The Automatic Voltage Regulator stabilizes the electrical output. It prevents power surges from destroying your sensitive facility equipment. Visually confirm the AVR module sits securely on its mounting bracket. Check its delicate wiring harness. If the AVR hangs loose by its wires, you must reject the unit or request an immediate field repair.
Visual and static checks only tell half the story. You must run the machine to prove it works. A proper 12 kW diesel generator quality inspection requires live testing. This phase separates reliable equipment from poorly assembled units.
Begin with a no-load startup. Document how easily the engine cranks and catches. It should start within a few seconds. Listen carefully for abnormal mechanical clanking or metallic scraping. Observe the exhaust smoke color immediately.
A brief puff of dark smoke is normal during a cold start. However, sustained black smoke indicates unburned fuel. Sustained blue smoke indicates the engine is burning oil. Once running smoothly, check the baseline voltage and frequency stability on the controller display. They should lock in firmly at your required specifications (e.g., 230V / 50Hz or 120/240V / 60Hz).
Running a diesel engine without a load causes "wet stacking," which damages the exhaust system. You must apply a synthetic load to prove the machine generates its rated output. Explain this necessity to your team. Connect a portable load bank to the output breakers. Apply the load in tiered steps. This verifies the unit can sustain 12 kW continuously without overheating or experiencing severe voltage drops.
Table Title: Standardized Tiered Load Testing Schedule
Load Step | Percentage | Duration | Inspection Focus |
|---|---|---|---|
Step 1 | 25% Load | 15 Minutes | Verify basic engine stability and initial temperature rise. |
Step 2 | 50% Load | 15 Minutes | Check for smooth turbocharger spooling and exhaust clarity. |
Step 3 | 75% Load | 30 Minutes | Monitor voltage regulation and alternator heat dissipation. |
Step 4 | 100% Load | 60 Minutes | Confirm sustained 12 kW output without safety shutdowns. |
Best Practice: Always record the oil pressure and coolant temperature at the end of each load step. This data provides a crucial baseline for future maintenance.
Modern generators utilize protective safety shutdowns. You must verify these sensors actually work. Safely simulate a fault, or use the controller's diagnostic mode to test the alarm circuits. Verify the engine shuts down instantly if it detects low oil pressure. Confirm the high-temperature alarm triggers correctly. These sensors act as the last line of defense against catastrophic engine failure.
The physical inspection represents only part of the receiving process. You must secure the paperwork to protect your investment. Missing documentation can void your warranty and complicate future technical support requests.
Never trust the outer shipping crate label. Locate the physical metal dataplate riveted to the engine block. Locate the second dataplate on the alternator housing. Match these exact serial numbers and output ratings to your original purchase order. Cross-reference them against the shipping manifest. Ensure the manufacturer shipped the exact voltage and frequency configuration you ordered.
Quality manufacturers provide proof of compliance. Ask the driver or supplier for the factory test reports. Look for independent compliance certificates. SGS inspection reports or ISO certifications carry significant weight. These documents prove an authoritative body validated the manufacturing process before the unit left the factory. Do not accept a unit lacking standard compliance paperwork.
Your inspection protocol directly supports your warranty rights. Document the entire receiving process. Take clear, date-stamped photos of the unit from all four sides. Photograph the dataplates. Log the initial hour meter reading. Record the results of your load bank test. Consolidate this evidence into a digital file. This establishes an undeniable baseline if you ever need to file a warranty claim.
A disciplined receiving inspection bridges the gap between capital expenditure and reliable backup power. Skipping these steps exposes your facility to unnecessary risks and hidden defects. By executing visual structural checks, verifying mechanical integrity, and demanding a rigorous load bank test, you secure your investment.
Take immediate next steps to finalize the process. First, formally accept the freight only after the unit passes all tests. Next, transition the machine directly into your facility's preventative maintenance software. Finally, schedule the first oil change immediately after the initial break-in period. Proactive management guarantees your power systems will perform flawlessly when you need them most.
A: Immediately document the damage on the bill of lading before the driver leaves. Take clear, date-stamped photos. Differentiate between cosmetic scratches and functional damage. Contact your supplier right away to report the issue. Do not refuse the shipment for a minor paint scratch, but do require written acknowledgment from the carrier.
A: No. Factory reports only prove the unit worked under perfect conditions there. Transit involves heavy vibrations, temperature shifts, and physical shocks. On-site load bank testing proves the machine survived transit safely and functions properly within your specific facility environment.
A: The standard timeframe spans 1 to 2 hours. You should run the unit under varying tiered loads, peaking at 100% capacity. This duration allows the engine block to reach total thermal stability. It also provides enough time to identify delayed fluid leaks that only appear under pressure.